Dragée Coating Is Uneven: Diagnosing Coverage Problems
Flat spots, doubles, rough shells or colour streaks in dragée panning? Diagnose each defect by root cause (charge size, pan speed, core shape, temperature and drying) and fix it.
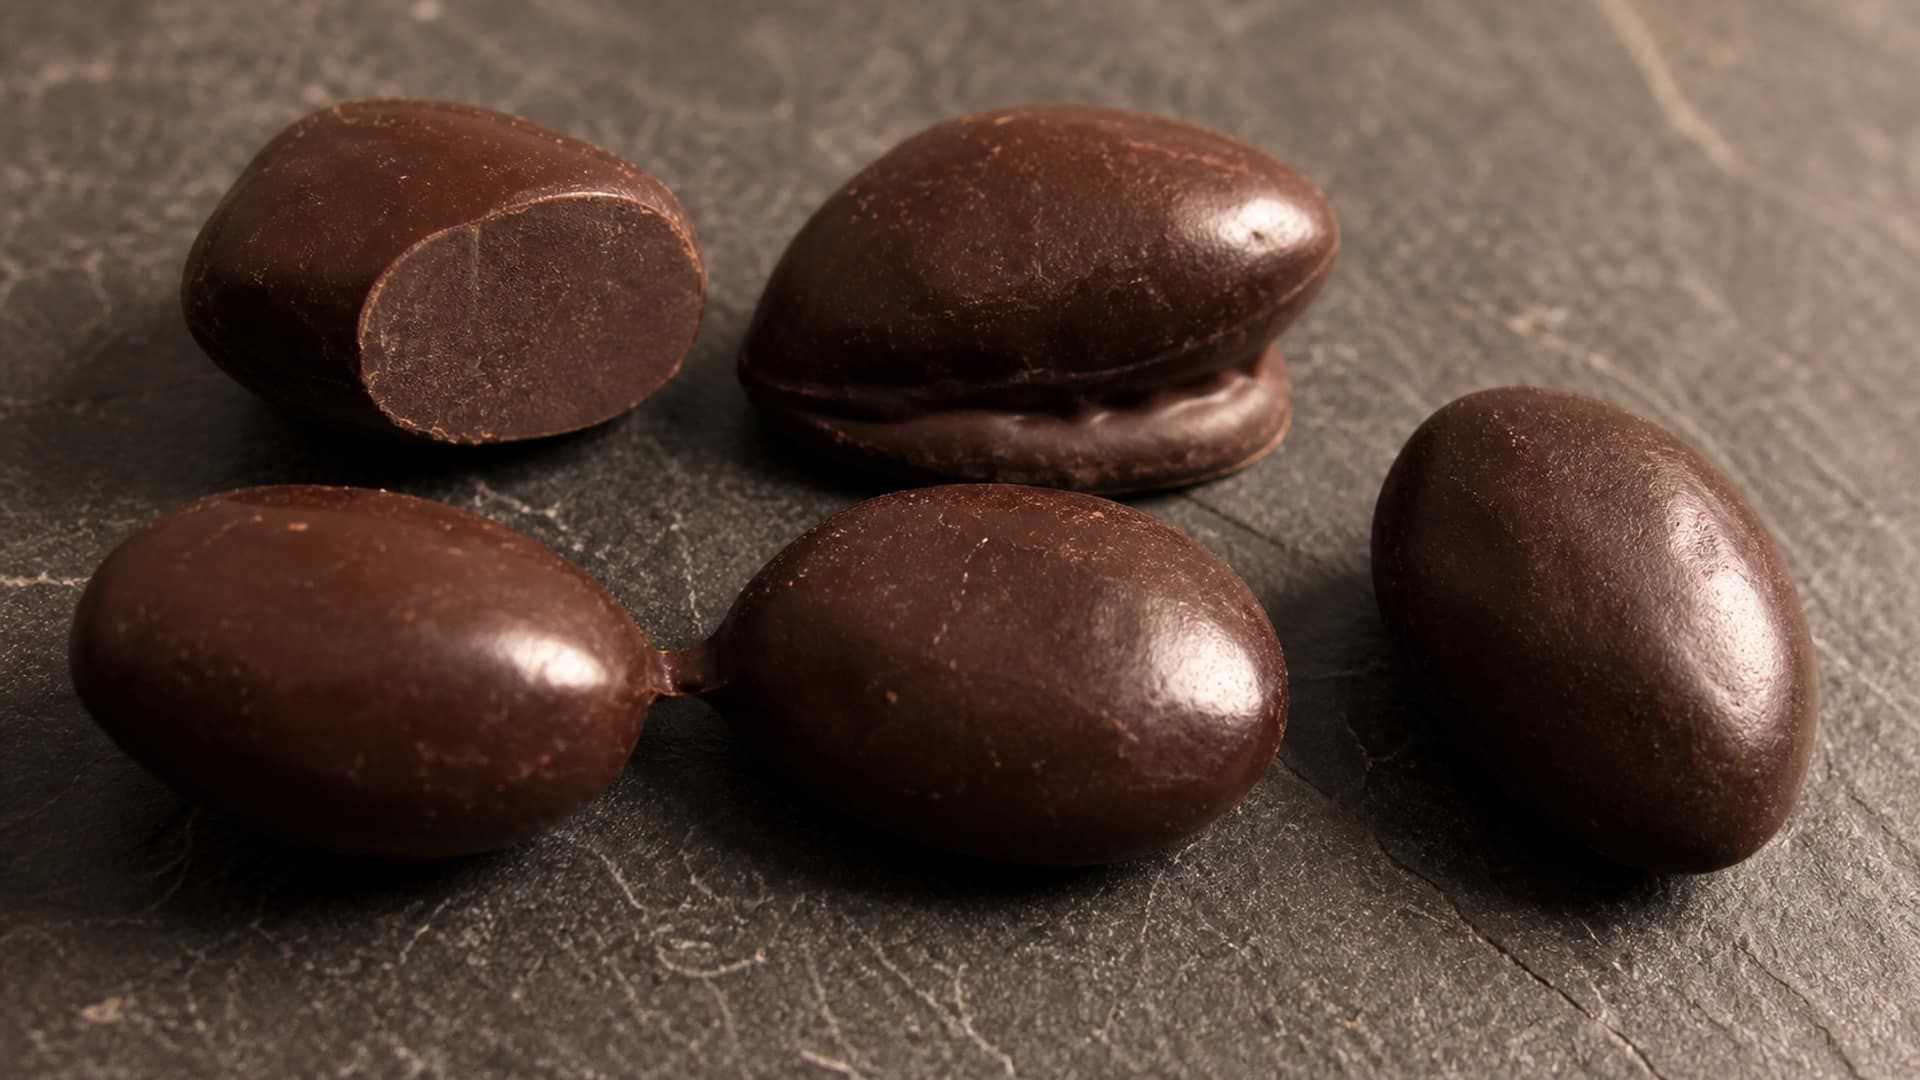
What Uneven Coating Looks Like
You pull a batch from the pan and something is wrong. Some pieces carry a lumpy ridge on one side, others look almost bare underneath, and a few have fused into pairs. Uneven coverage is one of the most common panning faults, and it can almost always be traced to a single process variable.
Each pattern points to a different cause. Identify the defect you are actually seeing before you change anything, because the wrong adjustment makes the problem worse.
| Defect | What You See | Primary Root Cause | Secondary Cause |
|---|---|---|---|
| Flat spots | One side of the piece has a thin, matte coating; the opposite side looks normal | Pan speed too low: pieces slide as a mass instead of tumbling | Core shape too flat or angular |
| Pooling / thick patches | Lumpy coating concentrated on one area of the piece | Charge too large for the batch, or pan speed too low | Syrup too viscous (too cool or too concentrated) |
| Doubles (bridging) | Two or more pieces fused together by coating | Charge too large, or the next charge added before the last one dried | Pan overfilled, so pieces cannot move freely |
| Rough / granular surface | Visible sugar crystals or a sandpaper texture instead of a smooth shell | Charge too small to wet every piece, or syrup crystallising on contact | Syrup too concentrated for an open pan (above about 75 Brix), or drying air too hot |
| Chipping and wear | Shell flaking at edges and points, dust in the pan | Shell over-dried between charges and turned brittle | Pan speed too high for the piece size |
| Colour streaks | Uneven shade that appears after drying or storage | Surface dried so fast it set glassy and released moisture later | Colour charge onto a damp surface; pigment not fully dispersed |
| Edge buildup | Coating thicker on edges and corners than on the faces | Flat or cubic core geometry catches coating on its edges | Charge too large for the shape |
Dragée Coating Defect Identification Guide
Diagnose Before You Adjust
Take 10–15 pieces from the batch and examine them under good light. Count which defect appears most often. Change only one variable at a time: if you change pan speed and charge size together, you will not know which one fixed it.
Cause 1: Pan Speed Too Fast or Too Slow
Pan speed decides whether pieces tumble freely and expose every surface, or slide and pool. Conventional coating pans typically run at 12–30 rpm. Small pieces work better at the faster end, large pieces at the slower end, and large-diameter pans run slower than small ones because the surface speed the product feels rises with diameter.
Too Fast: Pieces Are Thrown, Not Rolled
When the pan turns too quickly, pieces are carried high up the wall and dropped. Impacts chip edges and wear away fresh coating, wet syrup builds up on the pan wall instead of the pieces, and you lose both yield and smoothness.
Too Slow: Pieces Pool at the Bottom
When the pan turns too slowly, pieces slide along the bottom as one mass instead of cascading. Syrup pools under the mass: the bottom of each piece gets thick, the top gets almost nothing. Flat spots and heavy pooling together are the classic sign of a pan that is too slow.
Setting Pan Speed
Start inside the 12–30 rpm working band, lower for large pieces and large pans, higher for small pieces. The almond dragée schedule runs a 60 cm pan at 12–16 rpm. Watch the bed for a minute after a charge: pieces should lift, cascade across the top and return underneath. If they slide as a block, speed up in small steps; if they bounce loudly or chip, slow down. Pan tilt matters too: pans are usually set at 15–25°, and larger pieces drift to the front while smaller ones go to the back, so adjust speed and tilt together until that size segregation is minimal.
Cause 2: Charge Too Large or Too Small
Each charge of syrup or chocolate has a short window to spread across every piece before it starts to set. Charge size is a balance: too small a charge does not cover every surface and leaves rough patches; too large a charge cannot spread before it sets, pools, and glues pieces into doubles.
For sugar hard panning, a charge of roughly 1–3% of the batch weight, 10–30 g of syrup per kg, is the working range. Start near the low end and grow the charge as the pieces grow, because every charge has more surface to cover than the one before.
| Coating Stage | Charge per kg of batch | Concentration | Notes |
|---|---|---|---|
| Gum arabic seal | 10–15 g of solution | 25–40% gum arabic | 1–2 coats; first layer, even coverage decides adhesion |
| Sugar engrossing (hard panning) | 10–30 g of syrup (1–3%) | 70–75 Brix | Start low, grow with the pieces; the almond schedule runs 20–30 g/kg |
| Sugar smoothing | 15–20 g of syrup | About 65 Brix | More dilute and slightly smaller than engrossing to fill the valleys |
| Coloured sugar (final layers) | 12–18 g of syrup | 60–65 Brix with colour | Thinner than engrossing to avoid colour bleed |
Charge Size by Coating Stage
How to Measure Charge Size in Practice
Weigh the ladle or syrup jug before and after each charge and divide by the batch weight in kg to get g/kg. Experienced panners dose by eye, but measuring during troubleshooting shows exactly what is going in. A load cell under the pan does the same job continuously and tells you when the batch has reached its target weight.
What one charge adds is easy to work out if you measure everything against the starting core weight. A charge of 20–30 g of 72 Brix syrup per kg of starting cores leaves 14–22 g of sugar, so each charge adds 1.4–2.2% of that starting weight. A 44% weight gain takes about 25 charges at 24 g/kg, which is how the almond schedule is built. If you instead dose 24 g per kg of the growing batch, the charges grow with it and 25 of them compound to about 53%. If you are pooling at the top of the range, cut the charge toward 10–15 g/kg and accept more charges. If the surface turns rough, the charges are too small to wet every piece; increase them.
Cause 3: Core Shape Is Unsuitable for Panning
Core geometry cannot be changed once you have the product, but knowing how shape drives coverage lets you adapt. Round and oval cores coat most easily because tumbling exposes every surface equally. The further a shape departs from a sphere, the more the technique has to change.
| Core Shape | Examples | Coverage Risk | Typical Defects | Technique Adjustment |
|---|---|---|---|---|
| Sphere | Chocolate centres, malt balls, hazelnuts | Low | Few, if pan speed is right | Standard panning parameters |
| Oval | Almonds, peanuts | Low to medium | Slightly heavier coating on the ends | Slightly slower speed, thinner charges |
| Elongated | Pecan halves, long almonds | Medium | Heavy ends, thin sides | Slower speed, smaller charges, more of them |
| Flat disc or tablet | Compressed candy centres, macadamia halves | High | Edge buildup, flat spots on the faces, doubles | Slow speed, smallest workable charges, longer drying |
| Angular or irregular | Coffee beans, raisins, cashews, pistachios | High | Dead zones in recesses, heavy peaks on edges | Seal with gum arabic first, then very thin charges |
| Cube or rectangle | Caramel cubes, cereal pieces | Very high | Thick corners, thin faces | Consider enrobing or shell moulding instead |
Core Shape and Coverage Risk Assessment
The basic problem with non-round cores is dead zones: grooves, recesses or flat faces that tumbling never exposes well. A coffee bean’s central groove traps coating while the curved back gets normal coverage, leaving a visible ridge along the groove.
Working with Irregular Cores
Seal irregular cores with gum arabic before any sugar or chocolate: one or two coats of a 25–40% solution at 10–15 g per kg of cores, each dried before the next. The tacky gum film anchors the first sugar crystals and evens out the surface. Very round or oily cores that will not tumble in a clean pan can be helped by precoating the pan wall with a little of the coating material to give them traction.
Cause 4: Syrup, Chocolate and Air Temperature
Temperature controls viscosity, adhesion and setting speed, three separate mechanisms that all change coverage. A temperature fault often looks like a pan-speed or charge-size fault, which is why it is so often misdiagnosed.
Too Cold: Coating Sets Before It Spreads
Panning syrups distribute well when they stay below roughly 200 cP, and a sucrose syrup thickens quickly as it cools. That is why a 72 Brix engrossing syrup is held near 80°C, so it reaches the pieces fluid. A syrup that has cooled in the jug, or a charge poured onto a cold product bed, thickens before it spreads: you get rough, granular coverage and pooled lumps.
Too Warm or Too Wet: Coating Never Sets
If the bed stays warm and damp, syrup keeps moving and pools before it sets, and pieces stay tacky long enough to form doubles. With chocolate, warm air or a warm bed stops the coating from setting at all, and the batch turns into a sticky, clumped mass.
| Coating Type | Coating Temperature at Application | Process Air | Notes |
|---|---|---|---|
| Sugar hard panning (70–75 Brix) | Syrup held near 80°C | Warm air, 35–45°C, for nut centres | Chocolate centres limit air temperature: around 21°C with dry air |
| Gum arabic seal | Solution cooled to about 40°C | Gentle warm air, 35–40°C | Dry to a matte, slightly tacky finish; over-drying weakens adhesion |
| Soft panning | Liquid syrup plus dry sugar charges | No direct airflow; room 21–27°C, 40–55% RH | Forced air only blows sugar dust around the room |
| Chocolate panning | Chocolate at about 40–45°C, usually untempered | Cool air, 12–16°C, at or below 45–50% RH | Reduce airflow for the final smoothing charges |
| Polishing | Glaze or wax at room temperature | 18–21°C, 35–45% RH | Slightly warmer and drier than chocolate-panning air |
Temperature Reference Guide for Coating and Process Air
Check Temperature Where the Charge Lands
Measure syrup or chocolate temperature at the ladle, not in the holding vessel, and keep the jug in a heated bath between charges. Most rough first layers come from a charge that cooled on its way to the pan.
Cause 5: Wrong Drying Between Charges
Each charge must be dry (sugar) or set (chocolate) before the next one goes on. A new charge on a tacky surface does not build a second layer: it re-dissolves the first and leaves a thick, uneven mix that cracks on drying. Drying can also go wrong the other way, and both errors leave marks.
Doubles almost always mean the pieces were still tacky when they touched. Once fused, they have to be broken apart, which damages both, or discarded.
Apply the charge
Ladle or spray the charge (10–30 g of syrup per kg for sugar engrossing) evenly across the tumbling bed. It should coat every piece within 30–60 seconds.
Let it distribute before drying
Keep tumbling without air for about a minute so the wet coating spreads and levels across the pieces.
Dry with conditioned air
Turn on the drying air while tumbling continues. In a conventional pan with warm air, a sugar engrossing charge on nut centres takes about 15–25 minutes; automated pans with conditioned air cycle in roughly 3–15 minutes.
Test before the next charge
Press two or three pieces together lightly: they must not stick. The surface should look dry and chalky-matte, and a dry bed sounds crisper as it tumbles.
Do not over-dry
Apply the next charge as soon as the test passes. A shell left to over-dry between charges turns brittle and chips, and the next charge adheres less well.
| Stage | Typical Drying per Charge | Drying Air | Sign It Is Ready |
|---|---|---|---|
| Gum arabic seal | 8–12 min | 35–40°C | Matte, no longer sticky |
| Sugar engrossing, conventional pan | 15–25 min | 40–45°C | Dry, chalky-matte; pieces do not stick when pressed |
| Sugar smoothing | About 20 min | About 40°C | Surface reflects light evenly |
| Coloured sugar | 20–25 min | 38–42°C | Even colour, no tack |
| Sugar charge, automated pan | About 3–15 min | Conditioned, dehumidified air | Set by the pan's cycle and checked by weight |
Drying Time Reference by Stage
Dry Air Matters More Than Hot Air
Hard panning relies on dry air: the same drying can be done with less air at low humidity or more air at higher humidity, but damp air slows every charge. Air that dries the surface too fast is also a fault. The syrup skins over in a glassy state, traps moisture, and releases it later as colour streaks. If drying times drift, check the humidity of the drying air before you change anything else.
Chocolate Panning vs. Sugar Panning: Different Rules
Chocolate panning and sugar hard panning use the same pans but opposite physics. Sugar panning removes water so sucrose can crystallise; chocolate panning removes heat so cocoa butter can set. A fix that works for one will often ruin the other.
| Parameter | Sugar Hard Panning | Chocolate Panning |
|---|---|---|
| How the shell forms | Water evaporates and sucrose crystallises | Warm chocolate cools and sets on the centres |
| Coating at application | Syrup near 80°C | Chocolate at about 40–45°C, usually untempered |
| Process air | Warm, dry air (cooler for chocolate centres) | Cool air, 12–16°C, at or below 45–50% RH |
| Main risk if too warm or damp | Pooling, slow drying, doubles | Coating never sets; greasy, clumped mass |
| Main risk if dried too hard | Brittle, chipping shell; glassy surface and later streaks | Rough surface that the final low-air smoothing step must level |
| Before polishing | Rest so moisture can equilibrate in the shell | Rest so the fat can finish crystallising |
Process Comparison: Sugar Hard Panning vs. Chocolate Panning
Panning Chocolate Is Usually Applied Untempered
Unlike enrobing, chocolate for panning is normally applied warm and untempered, and it sets on the centres in cool, dry air. Do not chase temper in the pan. Control the chocolate temperature, the air temperature and the humidity, then give the pieces a rest before polishing so the fat can finish crystallising. If the shell blooms later, see the article on chocolate blooming below.
Using the Formul.io Dragée Calculator to Plan Layer Build-Up
Uneven coverage is often a planning problem as much as an execution one. If you know how much coating each stage has to deposit, you can size the charges instead of guessing. The Formul.io dragée calculator gives you that mass from geometry; it does not count charges or schedule the run.
Describe the core
Pick sphere, cube or irregular, enter the median core diameter in mm, the core density and the batch weight, and select the core ingredient. Oval cores such as almonds are entered as a sphere of the same volume. The minimum and maximum diameter turn the piece count into a range.
Stack the layers by thickness
Add one layer per stage, each with its coating ingredient and the stage's total thickness. Engrossing, for example, goes in as one 0.5 mm sucrose band. The calculator works in bands: anything under 0.1 mm is an error, so do not enter individual charges.
Read layer and batch weights
For every layer you get volume and weight per piece and per batch, plus the core weight, total coating, machine loss and total batch weight. Divide a band's batch weight by the number of charges, then by the syrup's Brix fraction, to get syrup per charge.
Check the warnings
The calculator flags moisture-migration risk between the core and layers, wet layers next to dry ones, fat layers under water-based ones, thin or very thick layers, coatings too heavy for the core, and batches that overfill the pan.
Pre-Production Checklist to Prevent Uneven Coverage
- Pan speed verified: a cascading bed, not a sliding mass, at the planned speed and tilt
- Pan fill checked: about 40–50% of the pan volume, so pieces can move freely
- Batch weighed: an accurate starting weight so g/kg charges are right
- Charge size set: 10–30 g of syrup per kg for sugar engrossing, starting low
- Syrup temperature checked at the ladle: not in the holding vessel
- Drying air conditioned: temperature and humidity right for the coating type
- Dryness test agreed: press-and-look test, and a rule against over-drying
- Core shape assessed: gum arabic seal planned for irregular cores
- Chocolate stage: air at 12–16°C and the chocolate temperature checked before the first charge
Frequently Asked Questions
My coating looks fine during panning but defects appear after drying. What is happening?
Why do two or three pieces keep sticking together?
Why is my sugar coating rough and granular?
Can I rescue a batch with flat spots or pooling?
How many charges do I need to reach my target coating weight?
Do almonds, hazelnuts and macadamias need different settings?
Related Resources
Related Topics
Related Articles
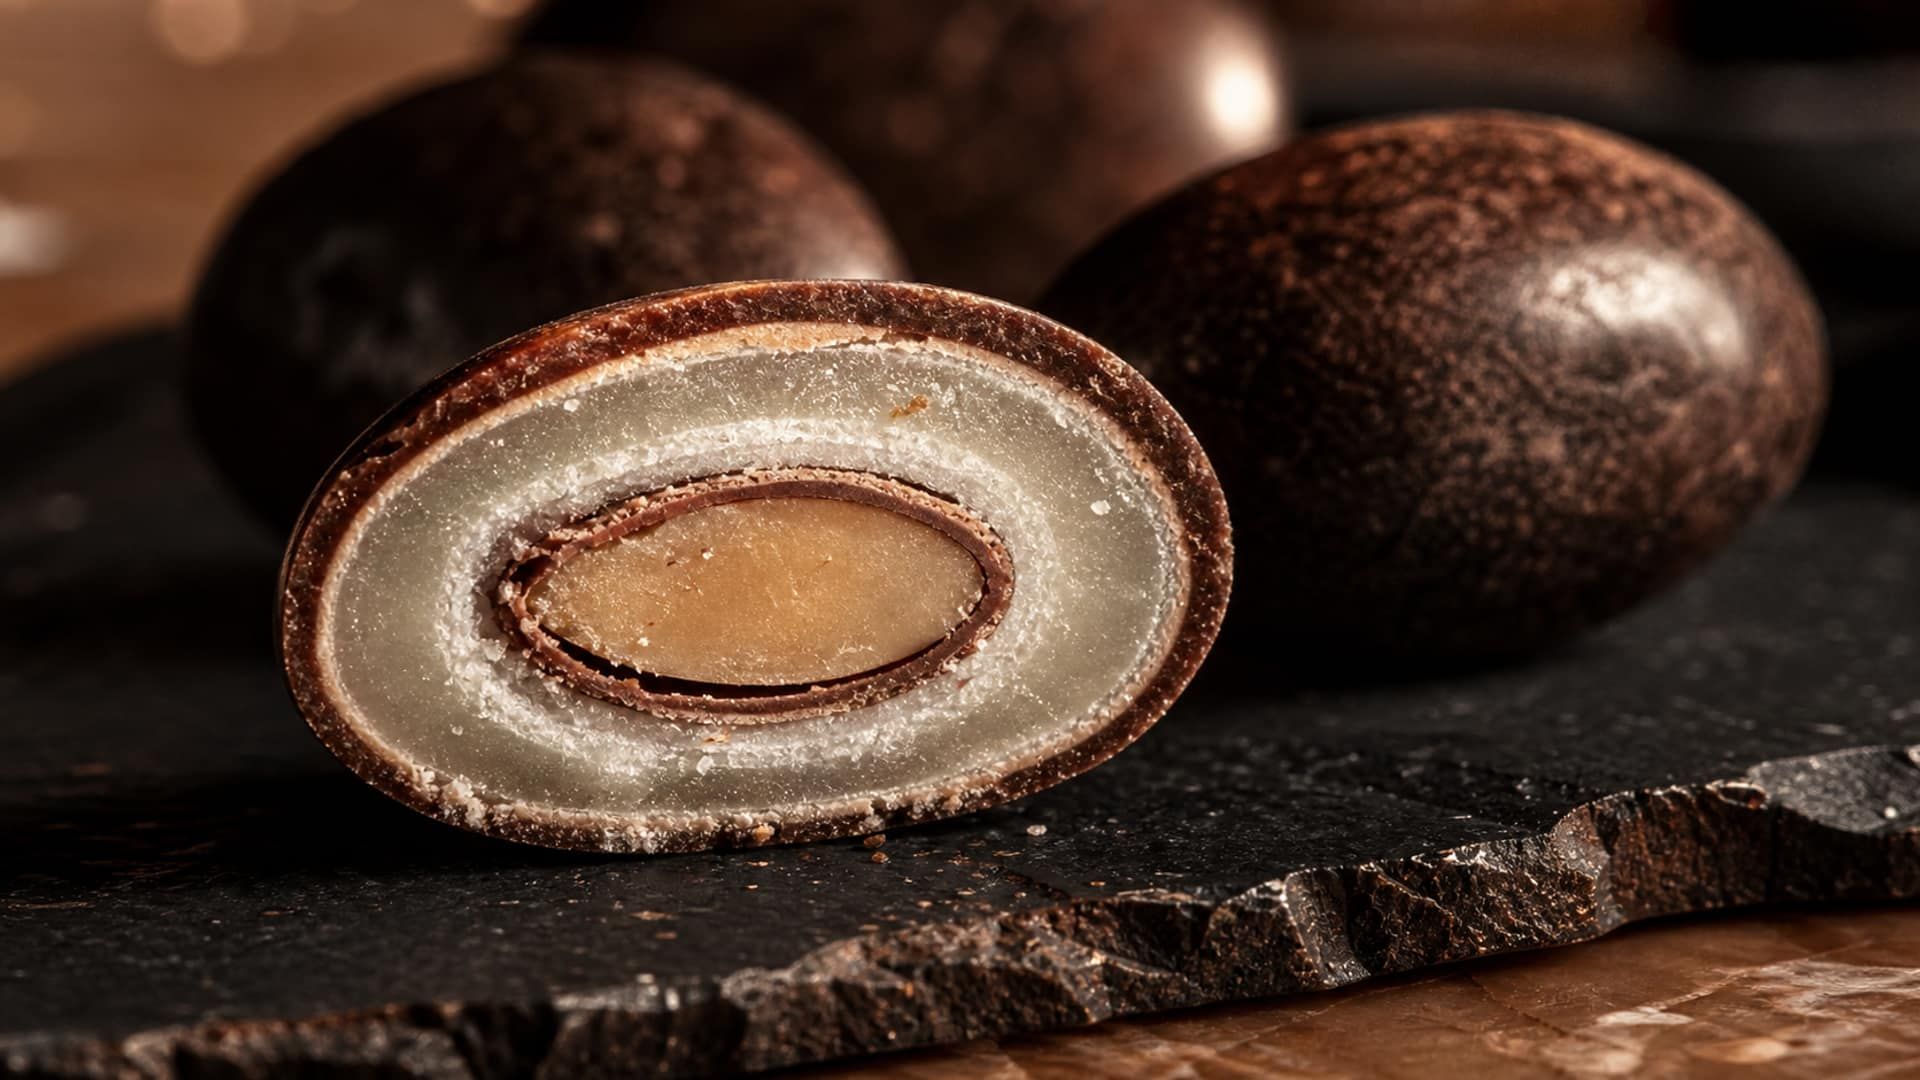
Dragée Coating Weight: How Much Coating Each Layer Needs
A coating layer weighs its shell volume times its density, and shell volume grows with the cube of the radius. How to calculate layer and batch coating weight for a dragée, with a worked sphere example.
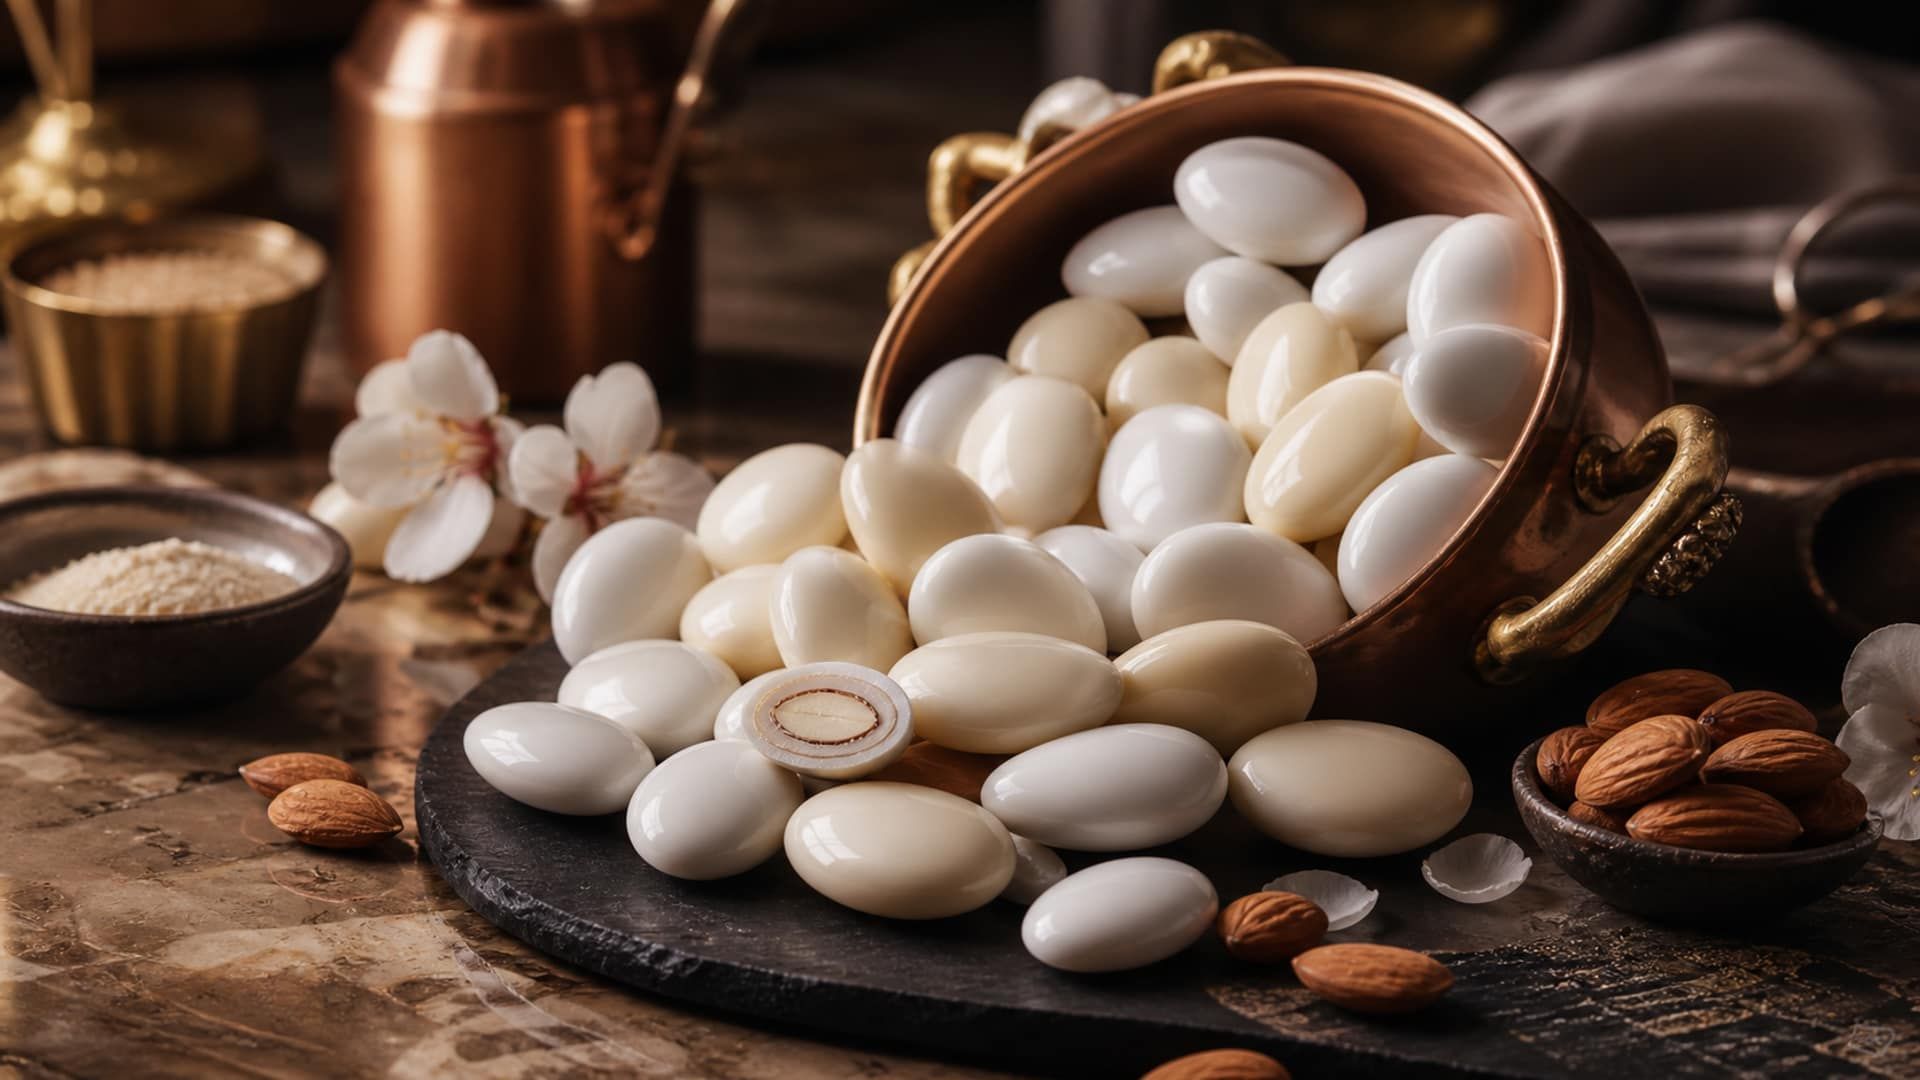
Almond Dragée: Building a Multi-Layer Coating from Core to Finish
A complete production guide to multi-layer sugar panning for almond dragée: gum arabic sealing, 20–30 engrossing layers, smoothing, coloring, and final polish — with calculator walkthrough.
Fat Bloom and Sugar Bloom in Chocolate: Diagnose and Prevent
Distinguish fat migration and polymorphic change from condensation-driven sugar bloom, then control temper, storage, and dew point.